Air separation · ASU
Air separation equipment defined around your production duty
IGS supports enquiries for cryogenic air separation plants and equipment across the UK and Europe. Requirements may range from a complete ASU or liquid-product plant to a cold box, heat exchanger, column, vessel, skid or plant-upgrade package.
Define the production case
Start with the gases you need to produce
Every ASU requirement begins with the production case: which gases are required, at what purity, pressure and flow, in gaseous or liquid form, and with what expectations for turndown, availability, energy use and future expansion.
IGS uses that production case to organise an initial technical review and define the appropriate equipment or project conversation.
Inside the ASU
Match the process cycle to the product mix.
Gaseous supply and liquid production place different demands on an air separation plant. The oxygen-to-nitrogen balance, delivery pressure and liquid output help define the compression and refrigeration arrangement.
Compression route
Internal and external compression arrangements are assessed against product pressure, liquid demand and the wider operating case.
Refrigeration balance
Air or nitrogen cycle options, compressors and expanders must be considered together with daily production and site electricity costs.
Additional products
Argon and rare-gas recovery can be considered alongside the main oxygen and nitrogen duty where the feed and process configuration support it.
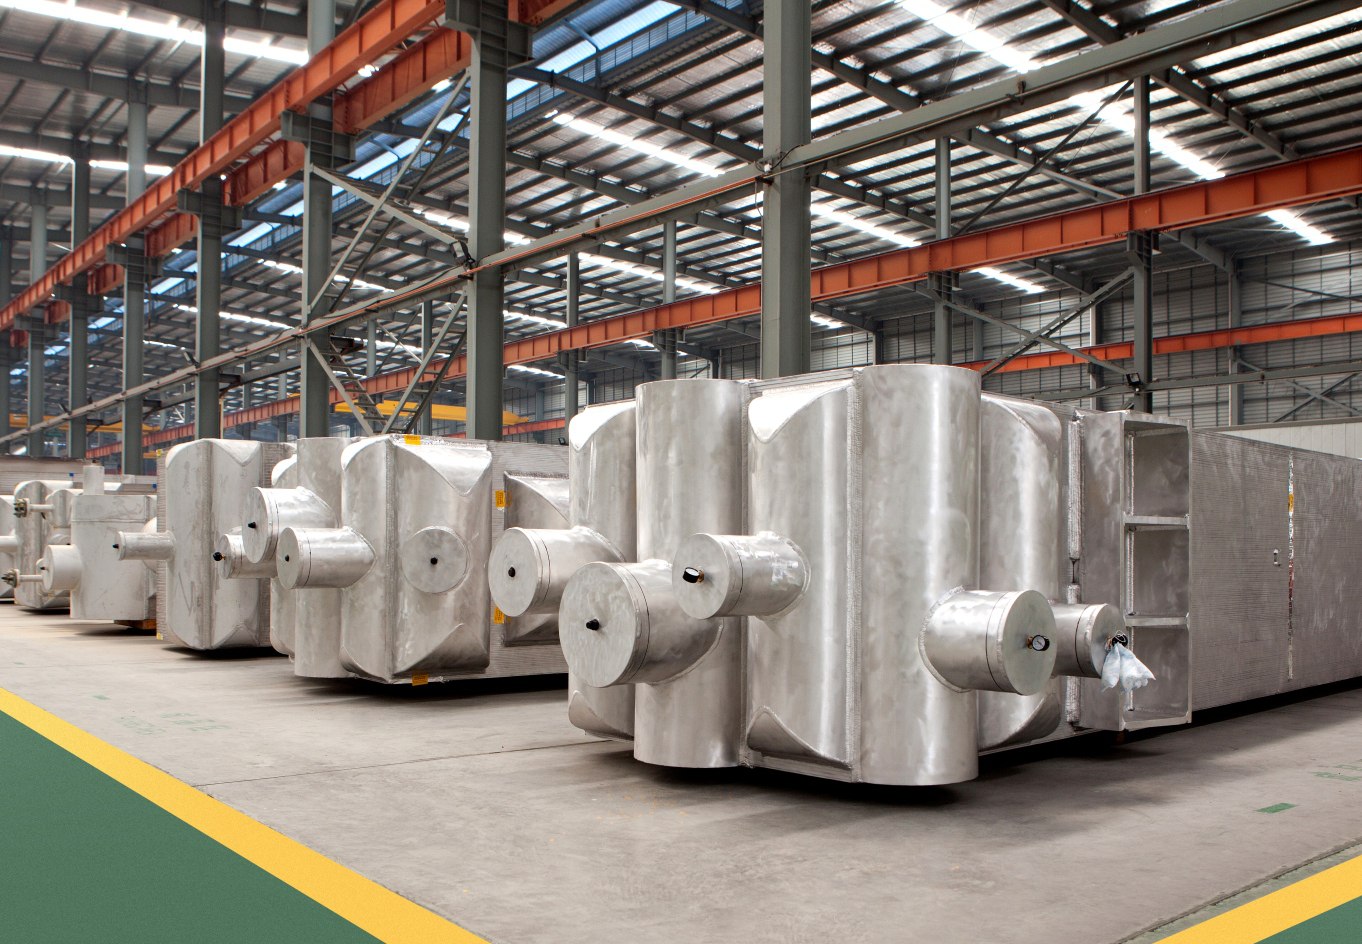
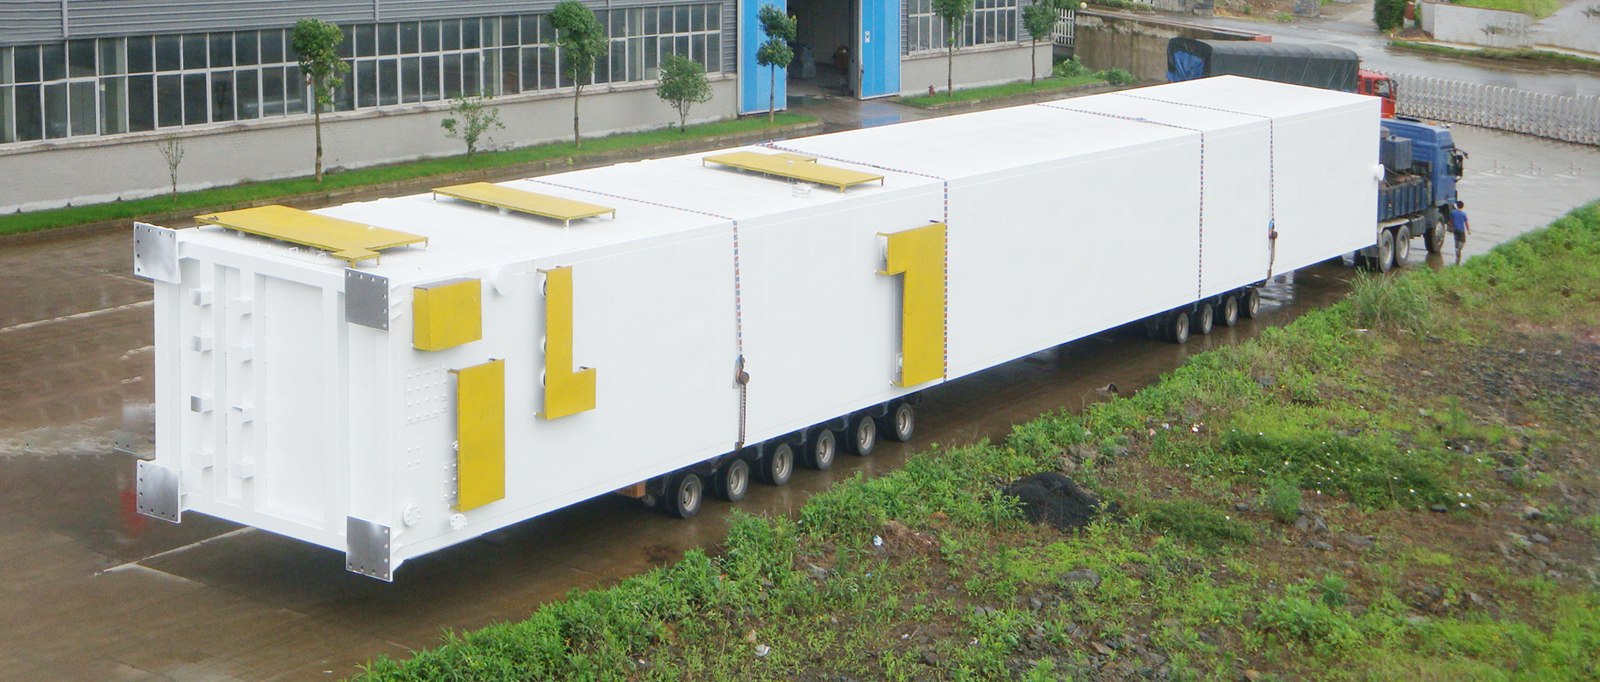
Equipment reference imagery from technical literature. Configuration and supply scope are defined for each project.
Discuss your ASU requirementEquipment and plant requirements
Typical ASU requirements
Cryogenic ASUs
Large-scale cryogenic air separation units for industrial and merchant gas production.
Liquid-product plants
Liquefaction and liquid-product ASUs defined around the required product mix and operating case.
High-purity production
High-purity nitrogen and oxygen, nitrogen and argon product configurations.
Integrated equipment
Cold boxes, plate-fin heat exchangers, distillation columns, cryogenic vessels and skid packages.
Rare-gas recovery
Recovery integrated with an air separation scheme where technically applicable.
Brownfield requirements
Modification, debottlenecking, efficiency or product-mix review, subject to site data and agreed scope.
Applications
Production shaped by the end use
Industrial gas production
Gaseous and liquid industrial gases for merchant supply, pipeline distribution or dedicated on-site use.
Steel and metals
High-volume oxygen, nitrogen and argon for process support, purging, inerting and refining.
Chemicals, refining and energy
Oxygen and nitrogen supply for chemical processing, refining, gasification and continuous duties.
Electronics and high-purity applications
Carrier-gas requirements where stability, purity control and supply reliability are central.
Information for review
What helps us review an ASU enquiry
Send the information you already have. If the project is earlier stage, start with the products, capacities and site context you are working towards.
- Required products and product state: gaseous, liquid or both.
- Target flow rates, purities and delivery pressures.
- Operating profile, turndown, availability and redundancy expectations.
- Site location, ambient conditions, utilities and plot constraints.
- Applicable design codes, client specifications and documentation.
- Project stage, target programme and commercial route.
- Existing plant data for modifications or upgrades.
Define the ASU requirement
Move from production case to technical review.
Upload a process basis, equipment data sheet, tender package or client specification—or begin with the best information available today.